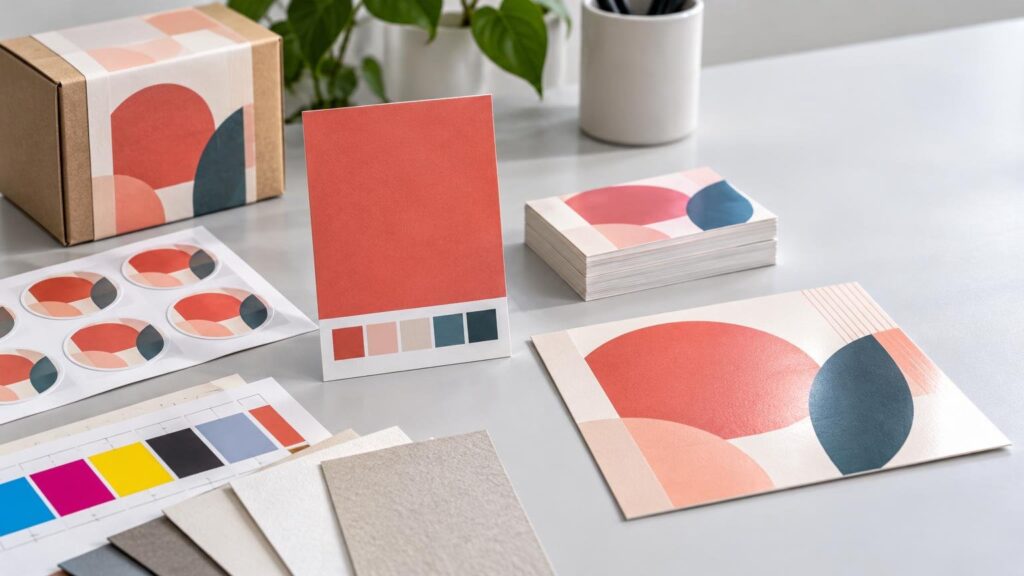
Keeping a brand color consistent across stickers, cards, labels, and invitations takes more than reusing the same logo file or CMYK values. Each product has its own printing condition: press or printer, ink set, substrate color, surface gloss, screening, coating, and sometimes white ink or a clear film. Change the condition and the same numeric recipe can produce a visibly different result.
The practical solution is to define the intended appearance, document how each product should reproduce it, and approve the right kind of proof. You may need separate production recipes for a coated card, an uncoated invitation, a white vinyl sticker, and a clear label even though all four represent the same brand color.
TLDR: Control the target, not just the color numbers
- Maintain one approved master color definition, ideally including a named spot color and a device-independent Lab target where appropriate.
- Keep source artwork tagged with the intended color profile, and record the profile used for every CMYK conversion.
- Treat spot ink and a CMYK simulation of that ink as different production specifications.
- Specify substrate, surface, coating, laminate, white ink, and print orientation as parts of the color condition.
- Use digital proofs for content and layout approval; request a physical proof or representative production sample when material and finish affect a critical color.
- Agree on viewing conditions and measurable tolerances before production when color accuracy is commercially important.
- Record the approved file, proof, construction, profile, color values, and tolerance so the next order can repeat the same target.
Start with a master brand-color target
A hex value is useful for screens, and a CMYK build is useful within a defined print workflow. Neither is a universal description of how a color must look. ICC profiles and characterization data describe how color behaves under particular device, ink, and substrate conditions. The International Color Consortium’s explanation of FOGRA39 illustrates this point: a characterization dataset represents a defined printing condition rather than every possible CMYK press result.
For an important brand color, keep a master record that identifies the approved swatch system and version. Add a CIELAB target or spectral data when a printer or color specialist can supply it. Lab describes a color independently of a particular CMYK recipe, while the output profile determines how that target is translated into printable values for a given condition. Our practical guide to Lab color in printing explains why that distinction matters.
Do not casually replace the master specification every time a vendor supplies a new CMYK build. Record that build as a product-specific recipe. It may be correct for one press and paper while being wrong for another.
Prepare source files for controlled conversion
Keep vector logos, named swatches, and editable color definitions in the master artwork. Embedded raster images should retain their intended profiles. Final production files should use the profile requested for the job, and any conversion should be documented rather than performed through an unknown export preset.
In a managed workflow, the output profile should match the intended device and paper condition. Adobe also warns against allowing both the application and printer driver to manage color, because that can apply unwanted double correction. This is primarily a production-provider concern, but buyers can reduce ambiguity by asking which profile, rendering intent, and conversion method will be used.
File construction still matters alongside color management. Supply artwork at final size, include the required bleed, protect important elements with a safe area, and use adequate image resolution. These checks will not make a brand blue more accurate, but they prevent resizing, clipping, and last-minute file rebuilding from introducing avoidable variation. A broader prepress workflow can catch these issues before approval.
Choose spot or process color deliberately
Process printing creates color from combinations of cyan, magenta, yellow, and black. A spot color is specified separately and may be printed with a dedicated ink. Some spot colors sit outside the reproducible gamut of a particular CMYK condition, so converting a named spot color to process does not preserve a guarantee of an exact visual match. Paper and ink behavior still affect a dedicated spot color as well.
Ask each provider whether the named swatch will run as an actual spot ink or be simulated with CMYK or another digital ink set. For short-run digital stickers, labels, cards, and invitations, simulation is common. In that case, approve the simulation as its own production target. If artwork uses spot colors with transparency, overprints, or effects, inspect separations and flattened output carefully; those interactions can change the final result.
Treat substrate and finish as color variables
Paper white is effectively the light source beneath most printed color. A bright coated card, warm uncoated invitation stock, opaque white vinyl, and clear label film therefore cannot be expected to return identical color from one shared CMYK build. ISO guidance identifies substrate color, gloss, process-ink color, screening, and tone-value increase among the variables defining a printing condition. ISO’s print-production guidance provides the technical framework behind that distinction.
| Product condition | Likely color consequence | What to specify |
|---|---|---|
| Coated cards | Higher surface smoothness and gloss can make color appear cleaner or more saturated. | Stock, coating, print condition, profile, and approved proof. |
| Uncoated invitations | Ink interaction and paper color can produce a softer or duller appearance. | Stock name, paper color, profile, and acceptable visual adjustment. |
| White vinyl stickers or labels | The white base supports opacity, but laminate can change gloss and contrast. | Vinyl, adhesive construction, laminate or coating, and print-side details. |
| Clear labels | The package color shows through unless white ink or another opaque layer is used. | Container color, white-ink plate, layer order, and surface-versus-reverse printing. |
Finish belongs in the same specification. Adhesive, secondary film, laminate thickness, curing, white ink, and surface-versus-reverse printing can alter clarity, gloss, and perceived color. This is why approving an unlaminated sheet does not fully approve the appearance of a laminated label. Review UV coating and lamination tradeoffs before selecting a finish solely for shine or durability.
When stickers or labels are part of the program, customstickers.com offers custom sticker and label materials that can be evaluated as part of the intended finished construction.
Use the right proof for the decision
A digital proof is efficient for checking artwork version, text, layout, trim, and general placement. It cannot reliably demonstrate the combined effect of screen calibration, production substrate, ink, coating, laminate, viewing light, and physical size. A physical proof or representative production sample is more useful when a critical brand color interacts with material and finish. The distinction is covered in more detail in the samples and physical proofs guide.
Even a physical proof needs a defined purpose. ISO 12647-7 contract proofs can serve as a visual aim for a stated printing condition. ISO 12647-8 validation prints have a different role and are not substitutes for contract proofs. For validation prints, the proof substrate should ideally match the production substrate; if that is impractical, gloss category and white-point requirements still matter.
For a multi-product launch, line up the approved samples under controlled, neutral lighting and also inspect them where customers will encounter them. Optical brighteners and fluorescent materials can shift differently as the ultraviolet component of the light changes. Fogra identifies paper color, gloss, and fluorescence as relevant material characteristics. Fogra’s paper-testing overview explains how those properties are evaluated.
Define acceptable tolerance instead of demanding zero variation
Consistency is controlled variation, not perfect numerical identity. ΔE00 expresses calculated color difference under stated measurement conditions, but it does not guarantee that every viewer will perceive two products as identical under every light. Measurement mode, instrument geometry, backing, substrate, gloss, and viewing environment all affect how a result should be interpreted.
Published ISO tolerances can provide context, but they should not be copied blindly into a purchase order. ISO 12647-8:2021, for example, specifies limits including an average applicable-patch ΔE00 of 2.5 and a declared spot-solid limit of 3.5 for its defined validation-print scenario. Those values describe conformance within that standard, not an automatic everyday tolerance for every sticker, card, label, or invitation.
Set a product-specific agreement instead. Identify the target, patches to be measured, instrument and measurement condition, backing, lighting, sample location, and tolerance. If visual approval governs, name the approved physical sample and define what differences in hue, lightness, gloss, or opacity would trigger review.
Build a repeatable brand-color record
A repeatable specification should travel with the campaign rather than living in one designer’s memory. Store the following information in a controlled brand-production record:
- Approved color name, swatch library, library version, and Lab or spectral target where available.
- Master artwork version, approved PDF, embedded profiles, output intent, and documented conversion workflow.
- Whether each product uses a true spot ink, process build, expanded-gamut simulation, or digital-device recipe.
- Substrate name and color, gloss category, coating, laminate, adhesive construction, white ink, layer order, and print side.
- Approved digital proof, contract proof, physical prototype, production sample, or signed reference sheet.
- Viewing-light and measurement conditions, including the selected ΔE00 method and tolerance when instrumental control is required.
- Printer, product, order date, production lot, and notes explaining any approved product-specific adjustment.
Then use a fixed approval sequence: lock the master target, confirm each production condition, receive profile and file instructions, convert deliberately, preflight separations, approve content, approve critical physical appearance, and retain the signed reference. For repeat orders, compare against that reference and document intentional changes rather than trying to reconstruct the target from an old invoice or screenshot.
The ordering takeaway
Do not ask four unlike products to share one unquestioned CMYK recipe. Ask them to reproduce one documented brand-color target through four controlled production conditions. Specify the files, profiles, ink strategy, substrate, finish, proof, viewing method, and tolerance. That turns “make the colors match” from a vague request into a repeatable prepress and quality-control plan.
References
- What is FOGRA39? — International Color Consortium
- Understanding color management, Adobe Acrobat | Adobe Acrobat
- Guidelines for using print production standards v2 Jan 2024
- Print with color management in Illustrator | Illustrator
- Artwork & File Setup Guide – Printiverse
- Spot vs Process Colors | Creative Cloud
- White Ink as a Color-Management Variable
- Samples And Physical Proofs – Printiverse
- SIST ISO 12647-8:2022 – SIST ISO 12647-8:2022
- Paper testing & specifications