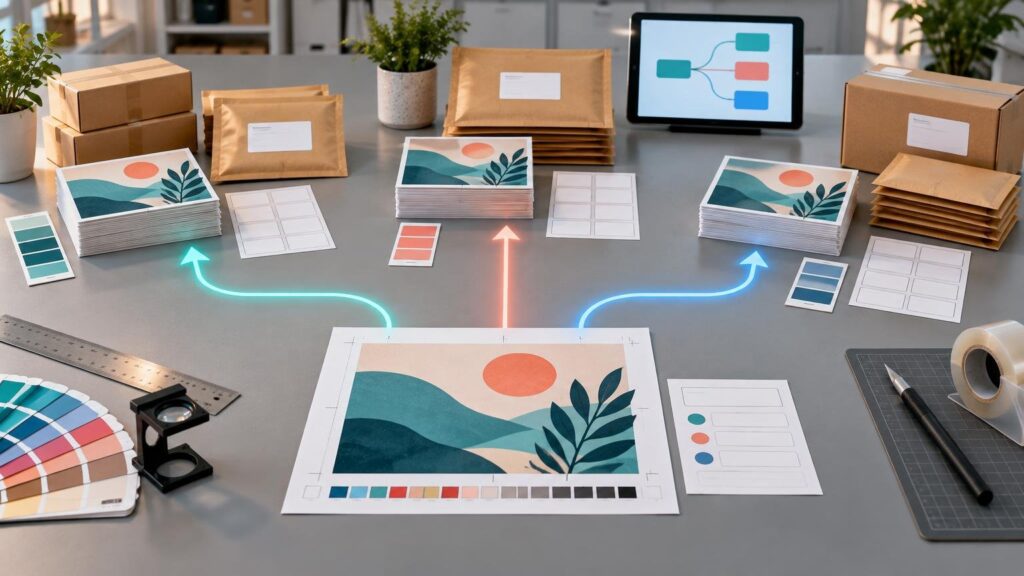
Custom distributed print services coordinate orders across one or more production facilities, often routing each job according to destination, capacity, equipment, inventory or required finishing. The model can reduce long-distance movement of finished goods and support localized, short-run production. It also introduces a serious control problem: every approved file, substrate, color target, finishing step and shipping instruction must survive the route from storefront to delivery.
TLDR
Buy the production system, not merely the ordering portal. A credible distributed-print provider should explain where jobs can be produced, how routing decisions are made, which specifications remain consistent across facilities, how substitutions are approved, and who owns a failure. Before committing a full program, run the same controlled test job through multiple facilities and compare the physical output, packaging, tracking data and reporting.
What distributed print actually means
In the model described by FESPA’s overview of distributed printing, digital files can be sent to production sites nearer the locations where the finished pieces will be sold or used, rather than printing everything centrally and shipping it onward. That can support shorter runs, regional versions and production based on current demand instead of a warehouse full of finished pieces. The result still depends on the capabilities and controls of the particular network.
Distribution does not always mean that every order goes to the closest plant. A routing system might send one job to a single facility serving several destinations, split it among regional facilities, or reserve specialized work for the only plant with the required press or finishing equipment. Some programs also coordinate recurring jobs, packaging and delivery so multiple documents arrive together.
This is different from ordinary print fulfillment. Printing creates the pieces; fulfillment can include receiving, inventory, picking, kitting, packing and shipping. A provider may be strong at one and limited at the other. Buyers planning multi-component packages should map the complete print fulfillment and kitting workflow rather than assuming a web-to-print storefront controls everything downstream.
Choose the operating model that fits the job
| Operating model | Best fit | Main control risk |
|---|---|---|
| Central production, distributed delivery | Consistent products with efficient production at one plant | Longer outbound shipping lanes and greater dependence on one facility |
| Regional production network | Localized pieces, recurring orders and geographically dispersed users | Variation among presses, materials, finishing and plant procedures |
| Hybrid routing | Programs mixing standard products with specialized finishing or inventory | Complex handoffs and unclear responsibility when components converge |
| Print plus fulfillment | Kits, replenishment programs and coordinated multi-item deliveries | Weak inventory data or disconnected production and warehouse systems |
The best model follows the physical job. A simple flyer may transfer easily among qualified digital presses. A package containing a folded insert, die-cut label, convention badge and prepacked promotional item has more dependencies. Routing that saves transit time on one component can create another shipment, an extra assembly handoff or a missed event date.
Inspect the production controls behind the portal
A polished storefront proves that orders can enter a system. It does not prove that each plant will produce equivalent output. Ask the provider to document the approved manufacturing specification: finished size, substrate by manufacturer and grade where necessary, ink or toner process, color targets, coating, lamination, cut tolerance, fold sequence, packing quantity and labeling format.
FESPA notes that decentralized suppliers may differ in materials, blanks, processes, commercial terms and quality-control practices. “Equivalent stock” is therefore too vague for a color-critical program. Two sheets with similar basis weight can differ in caliper, coating, white point and stiffness. Those differences can change color appearance, folding behavior, opacity and how the finished piece feels.
Color certification can indicate that a facility has established process controls, but it is not a promise that every product from every plant will look identical. The Idealliance facility-certification framework addresses calibrated equipment, gray balance, neutral-tone curves, proof-to-press alignment and broader process control. Physical output can still vary with the substrate, marking technology, finishing, equipment condition and the controls applied to the particular product. For a deeper explanation of device-independent targets and press behavior, see this guide to LAB color in printing.
Follow the order beyond web-to-print
The operational blind spot often appears after approval. An industry commentary published by WhatTheyThink argues that many web-to-print implementations automate storefront ordering while replenishment, inventory, kitting, drop shipping and reporting remain in disconnected systems. The article was sponsored by Propago and written by its marketing director, so this is an attributed industry argument rather than an independent market study. It nevertheless identifies the right area for buyer scrutiny.
Request a process map showing each system and handoff from order submission to final delivery. The useful questions are concrete: When is inventory reserved? How are version numbers transferred to warehouse labels? Can a kit wait for all components without losing its delivery priority? Does tracking return to the ordering portal? Can the provider identify which plant, press lot and shipping carton produced a disputed item?
Questions to put in the buying brief
- Which facilities can produce each product, and what conditions trigger routing to a different plant?
- Are substrates and finishes identical across facilities? If not, which substitutions are permitted and who approves them?
- How are master artwork, local versions, expiration dates and user permissions controlled?
- What proof is supplied for the initial setup, and what happens when production moves to another process or facility?
- Which tolerances apply to color, cutting, folding, registration, quantity and finished dimensions?
- Can orders be consolidated for kitting or delivery, and where does that assembly occur?
- How are inventory, spoilage, reprints, back orders and obsolete versions reported?
- Who handles a failure involving more than one facility, and what records are available for root-cause review?
- Are production time and carrier transit reported separately?
- What charges apply for setup, storage, pick-and-pack work, split shipments, rush routing and system integration?
Pilot the network before scaling it
Use a representative test, not an easy sample selected to flatter the system. Include small type, neutral grays, brand colors, images with shadow detail, folds or cuts that reveal registration, and the actual packaging instructions. Send the controlled job through at least two likely production routes. Compare approved proofs with finished pieces under consistent viewing conditions, then inspect dimensions, finishing, counts, cartons, labels, tracking events and reporting.
Record the acceptable variation and escalation path in the service specification. If visual matching is critical, identify the approved proof or measured target rather than relying on “match previous order.” If delivery is critical, define production completion separately from carrier pickup and arrival.
The buying takeaway
Custom distributed print services work best when routing flexibility sits inside a rigid specification and traceable workflow. Your request for proposal should include a product matrix, approved materials, color and finishing targets, routing rules, substitution policy, proofing triggers, fulfillment steps, reporting fields and failure ownership. Start with a multi-facility pilot. The network earns the rollout only when the physical pieces and operational records remain controlled after the order leaves the storefront.