A reliable print fulfillment kitting workflow treats printing, inventory, assembly, packing and shipping as connected but distinct operations. The decisive control is identity: every component, revision, kit configuration and shipment must remain tied to the correct order. A beautiful press sheet cannot rescue a kit containing an obsolete insert, the wrong quantity or a label for another recipient.
TL;DR
Approve artwork before production, assign a unique identifier to every stocked component, receive printed goods against expected quantities, scan components into controlled kit builds, inspect the finished kit and release shipping data only after the kit passes. Connect the storefront, production and warehouse records wherever practical. If people must rekey orders or reconcile separate spreadsheets, the workflow has an avoidable failure point.
Map the job before printing begins
Start with a bill of materials, or BOM, for each kit. It should identify every printed and nonprinted component, required quantity, revision, substitution rule, packing material and shipping instruction. Separate the customer-facing kit name from the operational SKU. “New dealer welcome pack” is readable, but the warehouse also needs an unambiguous version such as DEALER-WELCOME-R03.
The proof is the artwork control point, not the warehouse’s permission to improvise. Printiverse’s proofing process states that approval covers artwork, text, layout, sizing and trim guidance, and that production waits when a revised proof still requires approval. Its file guidance also calls for final-size artwork, appropriate bleed and safe areas, correct version identification and 300 DPI raster files. For die-cut pieces, review the cutting method, tolerance and artwork setup before freezing the BOM.
The end-to-end control flow
| Stage | Primary control | Typical failure |
|---|---|---|
| Order release | Approved kit version and BOM | An old configuration enters production |
| Print production | Job ticket tied to component SKU | Correct art receives the wrong finish or quantity |
| Receiving | Count, identity and condition check | Shortages or mixed revisions enter stock |
| Storage | Defined bin location and inventory status | Approved and obsolete pieces become mixed |
| Kitting | Scan or verify each component against the BOM | A component is omitted or doubled |
| Pack-out | Final kit inspection and package label match | The right kit goes to the wrong recipient |
| Shipping | Carrier or postal validation and dispatch record | Incomplete address data delays delivery |
1. Release controlled production files
Lock the approved file, component SKU and revision together. The production ticket should also specify stock, color requirements, coating, folding, cutting and other finishing that changes component identity. A revised brochure is not merely a new PDF; it is new inventory that must not be confused with the previous version.
2. Receive finished components into inventory
Receiving should compare delivered cartons with the purchase order or production record, then record accepted quantity, damaged quantity, revision and storage location. Use quarantine status for pieces awaiting inspection. Do not make newly arrived stock available for kitting merely because a pallet reached the warehouse.
Container-level identification becomes valuable when jobs span multiple cartons or pallets. GS1 defines a logistics unit as a case, pallet, parcel or other composition created for storage or transport. Its Serial Shipping Container Code guidance explains how an SSCC can uniquely identify that unit and connect a physical scan with related information. A smaller operation can use an internal barcode scheme, but identifiers still need to be unique and consistently applied.
3. Allocate stock before assembly
Allocation reserves components for released orders without falsely reporting that the kits are complete. This distinction prevents one large order from consuming stock already promised elsewhere. The system should flag shortages before operators open cartons and begin assembly. Decide explicitly whether partial builds, substitutions or split shipments are allowed; none should be assumed on the floor.
4. Build and verify the kit
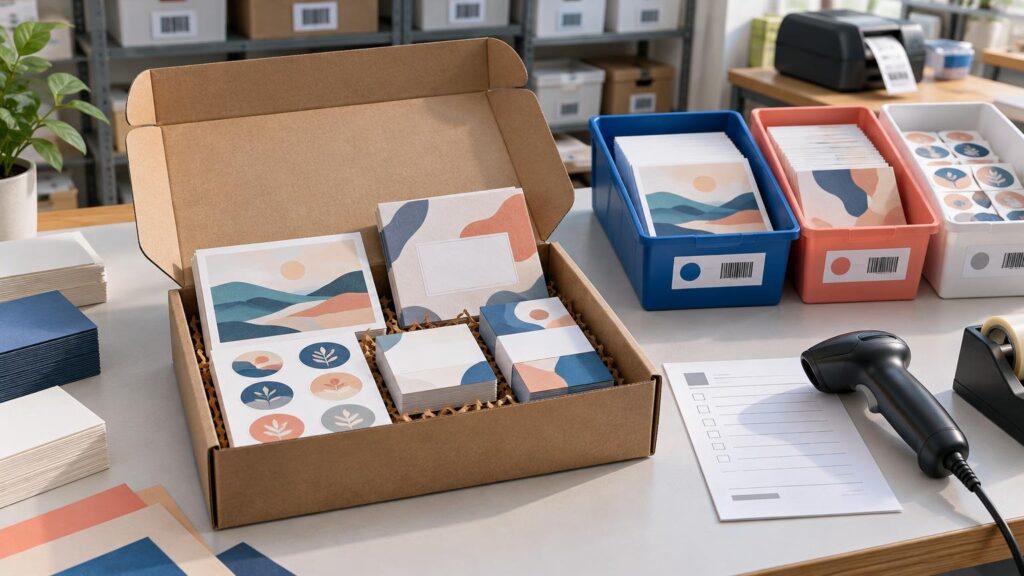
Set up the work cell in BOM sequence, ideally with one clearly identified component per location. Scan the kit order and each component where volume or version risk justifies it. Quantity checks can be manual, scan-based or weight-assisted, but the method must detect both missing and duplicated pieces. Record who completed the build and which component revisions were consumed.
5. Pack, label and release
The final check should confirm kit identity, component count, presentation, package type and recipient label. Keep the shipping label associated with the verified kit rather than printing a loose stack of labels for several open jobs. For mailed pieces, use the current USPS addressing requirements: USPS says an address must be complete and legible, and address placement can affect mailability, price and eligibility. Carrier transit remains separate from production turnaround and warehouse handling.
Connect the storefront to the warehouse
Web-to-print automation can stop too early. Sponsored commentary published by WhatTheyThink describes inventory, pick-and-pack, kitting, drop-shipping, replenishment and usage reporting as a downstream layer that may remain disconnected from order capture; separate data models can lead to exports and rekeying. Read the workflow analysis from WhatTheyThink. The practical lesson is to map every handoff, not merely install a storefront.
A connected workflow does not require one enormous software platform. It requires stable identifiers and defined exchanges among order management, production and warehouse systems. The CIP4 overview of JDF and XJDF describes a framework for exchanging product details, production details, operational data and device status across order entry, production, finishing and delivery logistics. Even when a plant does not implement JDF/XJDF, that model is useful: define which system owns each field and when status changes are allowed.
Measure errors where they originate
Track more than on-time shipment. Useful operating measures include inventory accuracy, component shortage rate, kits completed per labor hour, first-pass kit accuracy, damage rate, obsolete inventory and orders delayed by address or data exceptions. Record the stage where an error began. A missing insert discovered at pack-out may be a kitting error, but it may also trace back to a receiving shortage or an incorrect BOM.
Preflight the physical workflow
- Confirm that the approved proof, component SKU and revision agree.
- Create a complete BOM with quantities, finishing and substitution rules.
- Assign locations and status to received inventory before release.
- Test one complete kit using production components and packaging.
- Define scan, count and inspection points for assembly.
- Keep recipient labels tied to verified kits.
- Record component consumption, exceptions and shipment status.
- Reconcile remaining stock after the run and quarantine obsolete versions.
The ordering takeaway is straightforward: specify fulfillment as part of the job, not as an afterthought. Supply the printer or fulfillment operator with the BOM, revision rules, inventory ownership, packing sequence, destination data and exception policy before production begins. That turns kitting from a manual scramble into a controlled manufacturing step.